
Pneumatic pusher
Positive lateral removal for stable products with suitable spacing.
Track every failed pack from the inspection point and remove or contain it using a reject method suited to the product and line.
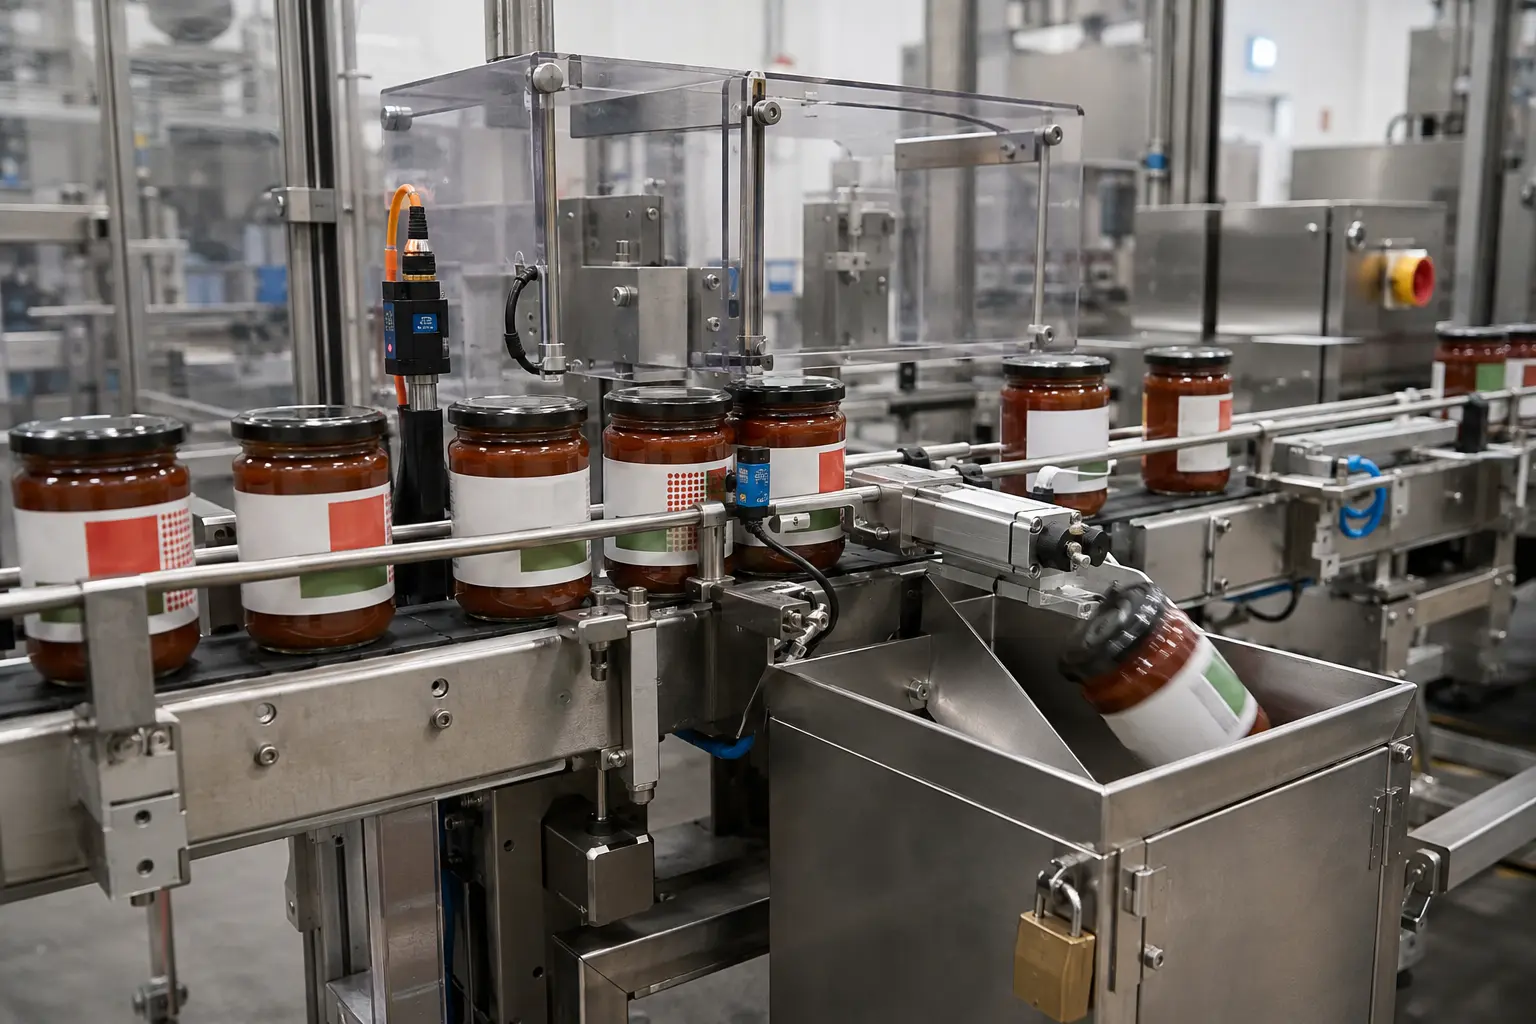
The controller associates the inspection result with the physical pack, tracks it to the reject point and confirms the expected action. The design accounts for pack speed, spacing, stability, weight and the consequence of a missed reject.
Positive lateral removal for stable products with suitable spacing.
Fast non-contact diversion for light products where containment is controlled.
Downward removal for unstable or difficult-to-push formats.
Controlled intervention where automatic removal is unsuitable.
Higher-risk applications can add assurance beyond a basic reject output.
A sensor confirms the failed product passed into the reject route.
Production is alerted before containment capacity is lost.
Pneumatic health is supervised where loss of pressure would defeat the reject.
Access-controlled containment supports controlled disposition of failures.